 WOBO Industrial Group Cryochains


Portable Ultra-Low Temperature Medical Freezer
Portable −86 °C Cryogenic Freezer for Medical and Research ApplicationsThe Portable Ultra‑Low Temperature Medical Freezer (−86 °C Class) is a specialized cryogenic storage unit designed for the safe preservation and transport of biological samples, vaccines, pharmaceuticals, and medical research materials. Engineered with advanced compressor technology, high‑density insulation, and precise digital controls, it maintains stable ultra‑low temperatures down to −86 °C. Compact and portable, the freezer is equipped with secure locking systems, ergonomic handles, and energy‑efficient operation, making it ideal for hospitals, laboratories, research centers, and field applications requiring reliable cold chain management.
You may also be interested in these products.
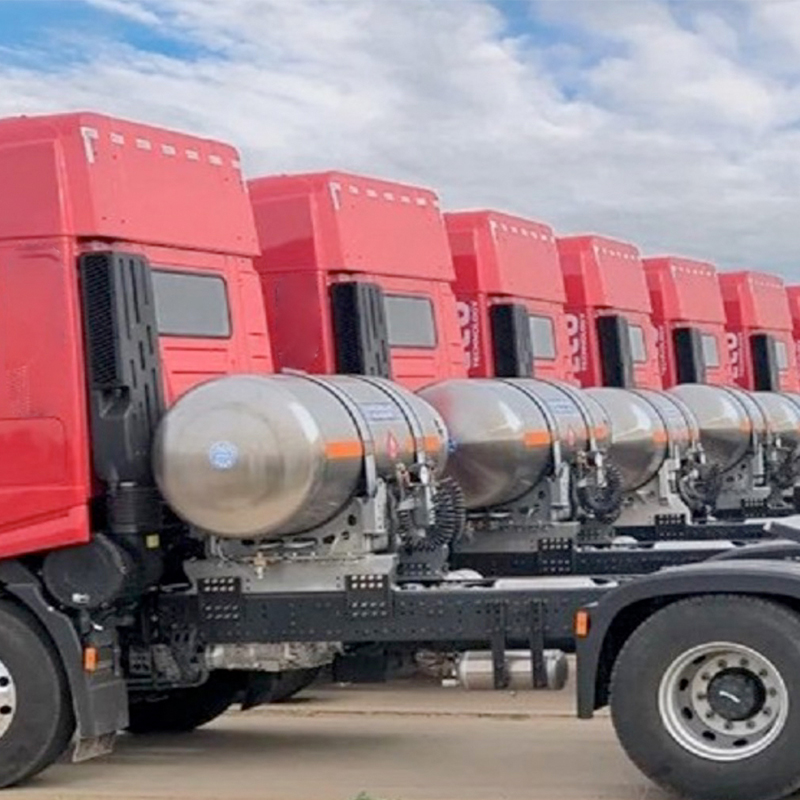
Onboard Liquid Hydrogen Tank
High‑efficiency onboard liquid hydrogen tank engineered for safe cryogenic storage and supply. Ideal for hydrogen vehicles, aerospace systems, fuel cells, and industrial energy applications.
Dry Ice Block Machine
High‑performance dry ice block machine engineered for industrial use. Provides automated CO₂ conversion into solid blocks with consistent quality, reliable output, and energy‑efficient design for food, medical, and logistics applications.
Cryogenic Liquid Storage Tank
The Cryogenic Liquid Storage Tank offers secure, efficient, and reliable cryogenic liquid storage with advanced insulation and stable pressure control. Perfect for laboratories, medical facilities, industrial cooling, and scientific research appli...
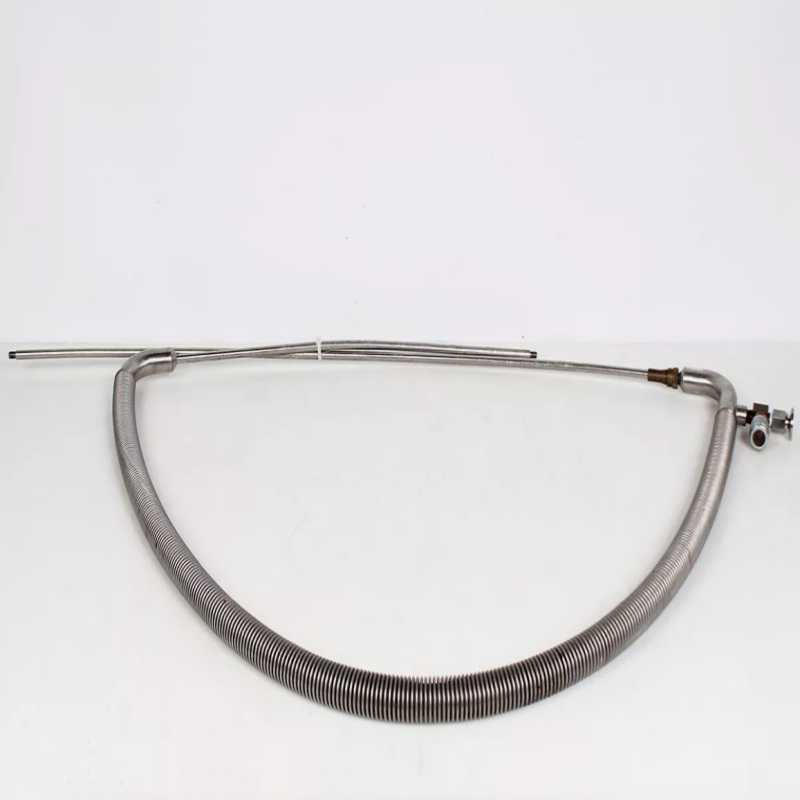
Liquid Helium Vacuum Insulated Hose
High‑efficiency vacuum insulated hose designed for low‑loss transfer of liquid helium. Ideal for superconducting systems, MRI facilities, laboratories, and advanced cryogenic research applications.
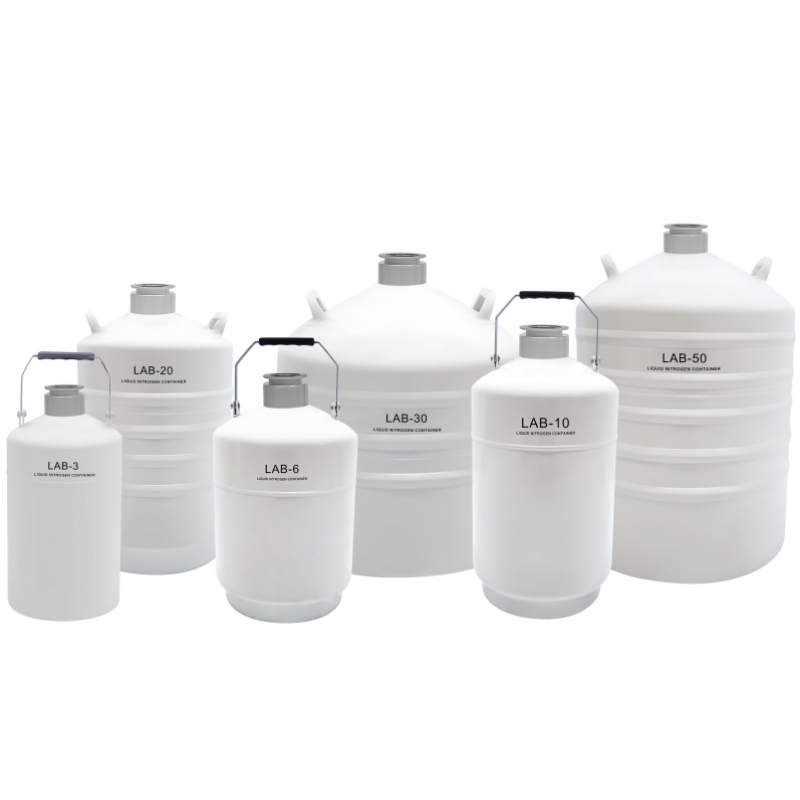
Laboratory Liquid Nitrogen Container
A durable, vacuum‑insulated laboratory liquid nitrogen container designed for safe, efficient, and low‑evaporation LN₂ storage. Ideal for research labs, medical facilities, biotechnology applications, and scientific testing.
Hydrogen Liquefaction Unit
High‑performance hydrogen liquefaction unit engineered for efficient conversion of hydrogen gas into liquid form. Ideal for aerospace, fuel cell technology, industrial energy, and advanced cryogenic applications.
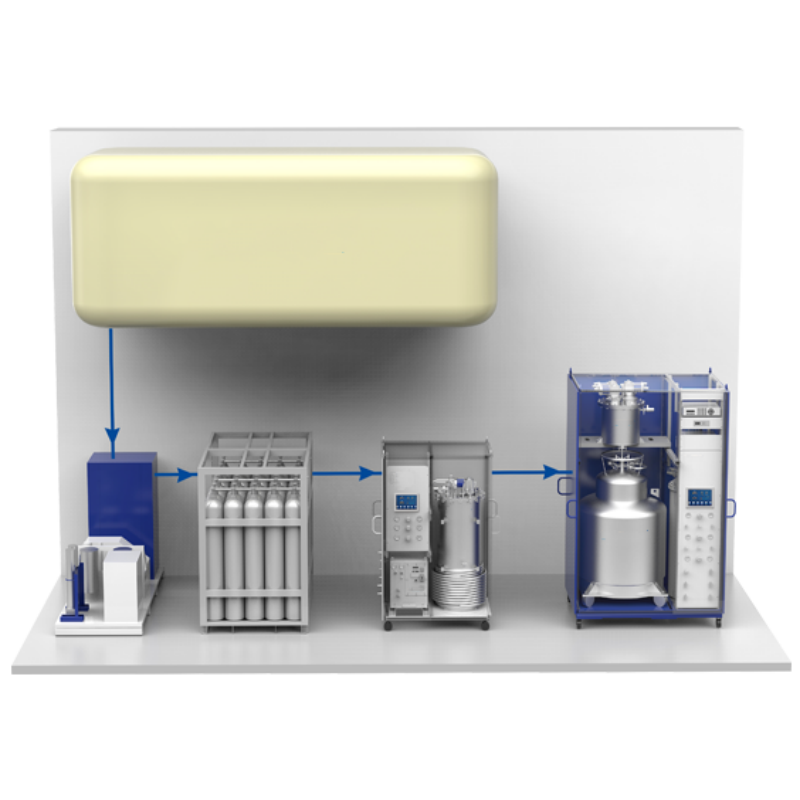
Helium Liquefaction Recovery System
High‑efficiency helium liquefaction recovery system designed to capture, purify, and reliquefy helium gas. Ideal for superconducting research, MRI facilities, and cryogenic applications requiring sustainable helium supply.
High-Pressure Piston Pump
Durable high‑pressure piston pump engineered for efficient liquid and gas transfer. Ideal for industrial, petrochemical, cryogenic, and energy applications requiring stable high‑pressure performance.




loading...
已经是到最后一篇内容了!